Aluminum foil is one of the most precisely manufactured thin layers of material used in modern packaging, but there is no foil roll that is completely uniform. In fact, the variation in thickness of aluminum foil occurs in every meter that is produced — in width, length, and from the edge to the center of the roll. The pertinent question for buyers and converters is not whether there is variation, rather how much variation is acceptable. The answer is that it depends on the purpose for which aluminum foil is being made.
In this article, we will explain what tolerances can be expected in different applications of aluminum foil as well as the standards that govern how those tolerances were established.
What does "thickness deviation" refer to
Prior to analyzing or discussing numbers, a definition of the two types of thickness variation that are present on a roll of foil is necessary:
- Gauge tolerance refers to the maximum allowable deviation of the nominal thickness measured based on a standard such as GB/T 3198, ASTM B479, or EN 546. The value that is found here is the one most frequently referenced, usually as a percentage (±4%).
- Transverse profile is the distance between the maximum thickness and minimum thickness computed across the width of the foil in one pass. Edge-to-edge variation is usually the reason behind certain problems such as defects in coating and lamination processes.
Both types of thickness variation are important, but while they might be considered equally important, they can lead to different consequences. A supplier that mentions excellent nominal tolerance but ships foil rolls of irregular transverse profile will cause a headache for the foil converter.
What the standards state
Aluminum foil industry standards that are most frequently encountered are:
- GB/T 3198 (China) — the national specification that most of the Chinese foil producers, HTMM included, manufacture.
- ASTM B479 (The USA) — governs foils used in flexible barrier materials.
- BS EN 546 (Europe) — harmonised European specification for rolled aluminum foil.
In general, for thickness up to the value of 0.05 mm (50 microns), the acceptable tolerance would be less than ±4% of the nominal thickness and gets tighter as the foil gets thinner. For heavier foil however, tolerances can be more relaxed but the high-end applications will require stricter tolerances.
Tolerance with respect of function
The amount of acceptable deviation decreases with the growth of the application. Some examples from different fields include:
Flexible laminates (6–9 μm)
Thin food packaging foil, such as sweet wrappers, coffee bags, and retort pouches, comes in thicknesses of between 6 and 9 μm. Tolerance is the most difficult at this point and is usually ±4–5% (around ±0.3 μm). Why is it so difficult?
At 6 μm, even a small change in the thickness can influence the barrier properties, as well as the increase in the chances for pinholes. A slightly thicker area will mean that the weight of 1 sq. m. of foil will be higher, which means money lost across hundreds of thousands meters of finished foil. It is also important to ensure the uniformity of the foil during high-speed laminating and printing process to avoid wrinkles and inaccuracies in printing.
Typical pharmaceutical blister foil is manufactured to a thickness of 20 μm - 30 μm with a margin of error of ±5%. The thickness of the foil does indeed play a major role in safety and quality as it helps in creating an efficient heat-sealed joint with the PVC/PVDC lid, thereby protecting the medicinal product from moisture and oxygen and allowing the foil to provide the pressure to break the bubble. Blister foils are also usually printed on both sides, making evenness of the foil even more important.
Household and food foils typically have a thickness of 30 to 80 µm and a margin of error of around 5 – 6%. Containers are created from deep-drawn foil, and therefore, thickness affects stiffness and rigidity of the foil and its capacity to retain shape without breaks.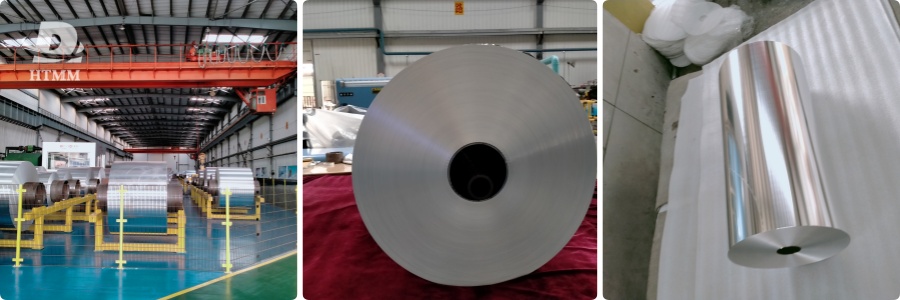
Heat-exchanger fin stock varying between 80 microns and 200 microns is an area where HTMM's 1xxx and 3xxx series alloys excel, with tolerances generally in the range of ±4–6%. The fin stock has to be absolutely uniform, as the fins are stamped and stacked in their thousands at a time. Non-uniform thickness disrupts the heat transfer of the entire coil and causes problems for the press tooling.
The significance of uniformity is greater than one might anticipate
Differences in thickness do not just refer to appearance. There are concrete, quantifiable impacts arising from thickness differences:
- Barrier properties – inconsistent thickness of foil means inconsistent protection from moisture, air, and light leading to shorter product shelf life.
- Cost and yield – extra micron in thickness means increased weight. An order of 500,000 m² gets its actual weight from changes in the average micron gauge.
- Downstream processability – laminate, print, coat, and convert processes work well only when the web is flat and uniform. Defective shape may result in your breaks, wrinkles, and waste.
- Ending product quality – packaging can’t be torn, blister can’t be broken, foil can’t be deformed.
How HTMM regulates this
HTMM Aluminum Foil has been involved in the manufacturing and shipping of food-grade aluminum foil for over 15 years, and the reliable gauge control contributes largely to the company's long-standing track record with customers. The company provides the various aluminum alloy materials, including grades 8011, 8079, and 1235, at thicknesses within the range of 0.006–0.2 mm, rolled in compliance with those of GB/T 3198 with minimal tolerances being maintained depending on the application type.
Full mill test certificates accompany each coil ensuring warranty claims on thickness match with actual inspections. When ordering aluminum foil, the question should not be whether it will be of the same thickness as any similar volume but whether its thickness will fit the needs, and this is something you can always discuss with us.