8011 aluminum foil master rolls easily mismatch all parameters without detailed confirmation, it is the most frequently overlooked cost accounting mistake of all various buying factory on the planet.
8011 foil buyers often pay all their consideration to the unit selling price ignoring the matching parameters need, and eventually cause truckload-like bad production accident of several million tons, material wastage of 3 hundreds tons, impure finished item quality with many unwanted pinholes, and several weeks' delay in the delivery schedule.In fact, 8011 alloy foil master roll is different from a batch of common raw materials and also an excellent semi-finished product that manufactured based on specific processing equipment, technical operation, and product application context.
Every technical indication should have thoroughly matched with the converting facility, technique, and finished item final stage application context exactly. This article will introduce in detail all of the standard technical parameters that must require confirmation of the real order, plus verification method and solution, to ensure you as an industrial player can avoid parameter mismatch, output optimized long-run benefit from roll to roll.
Order need to fully match final processing and application scene is the first key to ensure downstream processes have stable machine running.
.jpg)
8011 alloy with O temper is in the optimal softness, ductility, flexibility, and the finest ability to show up the processing performance, so it is the core component in the general purpose lamination and secondary converting operation in the flexible packaging field.
But if the final application scenario demands higher tensile strength and structural resistance for any specific application, the expensive titanium full hard H22, H24, or H26 tempers are often a better choice.
Then always make sure of the precise definition of foil thickness and allowable Thickness deviation, which directly influence the visual effect of composite, printing, and other secondary decoration.
The tolerances for the industry standard level are within 5%, but the foodstuff and pharmaceutical packaging industry cannot put up with this moderate tolerance.
The various gauges of 6 to 9um will meet the demand for ultra-lightweight portable pack products for food, nutrition, and household daily chemicals, while 10 to 30um is the best option for the medium-range flexible packaging and household foil product application scene.
Verify all key parameters of 8011 aluminum foil master roll to guarantee on-site operation after ordering.
The overall effective width of the aluminum foil roll must be consistent with the live width of the slitting equipment. If higher than the effective working width, it can lead to excessive edge material loss and higher processing costs; If narrower than the effective working width, it can lead to higher waste and waste rate during cutting.
The precise range of parameters also covers thickness, which should be specified based on the actual lamination process standard, the requirement for ultra-lightweight packaging or high-structure resistance package in outdoor heavy-duty applications.
Simultaneously specify the width and tolerance of master roll edge, which can effectively reduce the material loss of edge trimming and ensure the accuracy of overprint registration in multi-color lamination and printing process. Among them, the common tolerance of width is 1mm.
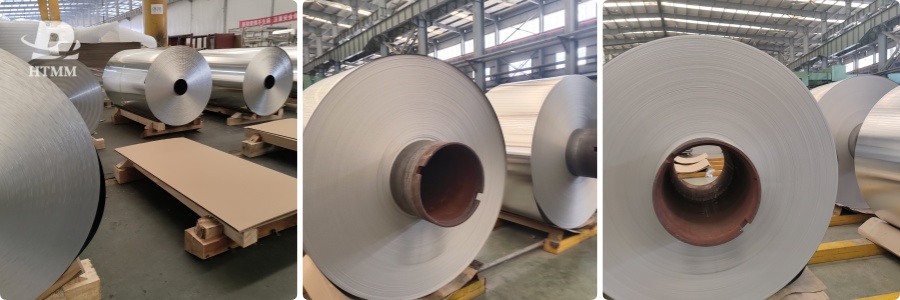
In addition, it also needs to specify the single roll weight, outer diameter, and core. The mainstream core of industrial production is 76mm and 152mm, which is the foundation of the subsequent slitting, rewinding process, and effective output.
Every parameter of master roll specification must be well matched with the on-site slitting and rewinding equipment, otherwise, it will be difficult to adapt to the rapid operation and unpredictable downtime.
Generally, the overall effective width should be well adapted to the effective width of the slitting and rewinding equipment. If the width is too wide, it will cause excessive loss; If it is too narrow, it will increase the number of rewinding, with more processing costs.
Meanwhile, specify the thickness according to lamination techniques and standards, 8011 hard foil in the appropriate thickness will provide a structurally resistant barrier for thick composite packaging or outdoor protective packing product.
All roll parameters of core size and outer diameter should well suit the corresponding requirements of rewinding equipment, and mismatch core dimension will risk unstable clamping and unstable rotation.
At the same time, determine the actual output number of rolls according to the requirements of final product output and the number of output of the entire market cycle, because the more single roll weight is, the less the labor cost of equipment change can be saved.
.jpg)
Specialized industry-oriented inspection of batch-to-batch quality should be carried out before ordering.
Among the indicators, thickness consistency and total quality consistency are the preconditions for on-site conversion and high-definition printing. Slight deviation will lead to the real-time tension fluctuation during the high-speed operation, easily leading to web deviation and breakage, and bring production downtime loss.
The rate of pinholes directly affects the barrier performance of aluminum foil surface, which is of great significance in prolonging food freshness, moisture resistance and delaying corrosion. For food packaging industry, the pinhole rate must be strictly checked, while the higher the industry standard requirement, the more strict the pinhole control.
In terms of surface quality, the residual oil content should be strictly controlled below 2mg/m to facilitate composite lamination and coating adhesion, and avoid degumming, peeling and composite damage phenomenon in finished products.
And the flatness, edge finishing, tightness of winding will directly affect the stable output in the process of high-speed cutting, and then cause the product edge wandering, jumping and so on phenomena.
Confirming all key indicators of 8011 foil master roll before formal order can save the indirect on-site production cost; At the same time, helps ensure the final product can be mass produced and delivered smoothly.
For example, it is better to be single roll capacity is as high as possible to reduce the frequency of equipment change; It can do minimum width tolerances of 1mm to achieve minimum waste during edge cutting.
Confirming quality indicators of batch consistency, pinhole rate, surface quality, and winding quality, use the seasoned supplier to get high-quality finished 8011 foils. In the long run, it can avoid equipment failure and operational interruptions.
Confirming the export packaging specifications of moisture-proof, waterproof, impact-proof, and wrinkle-proof will be necessary for long-distance ocean transportation and port handling to ensure safe delivery to each client in the global market.
Confirm the effective delivery cycle and stable production capacity of the whole year in advance, for the long-term order, the supplier should be able to keep the delivery and quality stable without breaking the order in different time periods.
Through the standard process of verification, ordering 8011 aluminum foil master rolls without specification confirmation is actually the most cost-effective method.
Sorting out the specification of each indicator, from alloy grade, temper, gauge, width, tolerance, core size, and specification to finish the pack as well as item limit inspection, try best to narrow down all parts with the supplier to get stabilized specification if long-term order in bulk volume.
(In the technical standard of general purpose flexible packaging and household foil products, it is recommended to choose O tempered alloy, 5% tolerance of gauge and width, 76mm or 152mm core diameter, non-tolerance core size, 1mm tolerance of rolled width, and less than 50 pcs single roll capacity.
For the high-grade foodstuff and pharmaceutical industry, the alloy grade must be confirmed before ordering; And specify the tolerance of gauge to 3% to see better finish product quality; And specify the core size within the tolerance range of the supplier instead of a fixed value; Confirm the order quantity based on single roll weight, and the single roll number can minimize the loss of trimming edge.)
Only after performing such standard specifications can the final benefit in the form of quality, cost, and delivery times be maximized.
Final words To optimize production and deliver the highest quality finished product, buyers should check from every individual element of roll specifications before ordering 8011 master foil roll.
These elements must be consistent with the application equipment standard, final application technique, and finished product standard.
We strictly recommend that these elements should be quantitatively defined and cross-vetted with the process run, including 8011 alloy alloyed grade, temper, alloy Gauge, allowable tolerance of Gauge and effective width, finished roll core size, maximum single roll weight, and effective roll weight.
The technical specifications of pinhole rate, and surface residual oil content must be strictly confirmed as well.
Obtain factory test reports and check through the inspection agency to make sure each production lot has no additional difference in specification compared to the corresponding preliminary quantity.
And confirm the standard pack format, standard export packaging specification, and delivery period for each order.
Only a unique process of confirming all specifications can the industrial user avoid ordering risk, and realize stable production and stable long-term benefit,