In a nutshell, the answer is affirmative—8011 aluminum foil is one of the best-known materials for the packaging of food and pharmaceutical products.
Its distinctive feature is the combination of the mechanical properties, barrier capabilities, and regulatory conformity that make this alloy the right answer to the need for protection of sensitive goods in these difficult spheres.
This publication identifies the basis for its applicability, its key application specifics, as well as the procurement recommendations that will provide you with the best decisions.
Basics of the suitability of aluminum foil 8011 in food and pharmaceutical packaging
Basic Characteristics and Application
Due to its outstanding ductility, formability, and processing performance, the 8011 aluminum foil is suitable for a variety of flexible packaging and container forming processes.
Its alloy composition has aluminum with the controlled addition of iron and silicon limiting points that are necessity for high-speed converting operations making 8011 the most widely used aluminum for food packaging, pharmaceuticals, and other commodities in the world.
Exceptional Barrier characteristics
8011 aluminum foil displays one of the most important characteristics of foils, which is the efficient barrier being able to protect from the penetration of light, oxygen or water vapor.
Moreover, it prevents the penetration of environmental factors from outside, making the quality of products stable and prolonging the custodianship of products like food and medicines.
This kind of protection from barriers is necessary to eliminate the influence of oxidizing, hygienically or photodegradation processes.
Safe for Using in Food industry
8011 aluminum foil of food production quality passes several tests regarding such indicators as the cleanliness of the surface, the presence of oil residues and contaminants.
Produced in compliance with ISO standards, it meets FDA and European Union standards of food safety and can contact food-stuffs of various compositions (acidic, fat and salinity).
Advantages of Pharmaceutical Packaging
8011 aluminum foil has moisture, light, and oxidation barriers that perform very well in the pharmaceutical industry.
It fits perfectly for blister packs, aluminum-plastic boards, and other forms of packaging that are used in this industry.
Its stable barrier performance fully meets the need for high freshness, stability, and quality of pharmaceutical products and allows keeping them effective for the entire shelf life.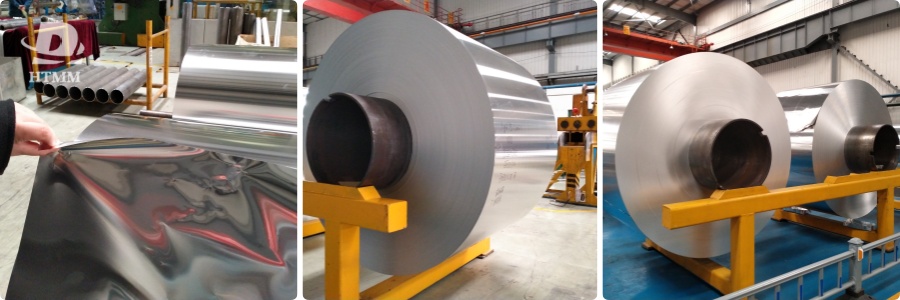
Food Packaging Applications of 8011 Aluminum Foil
Types of Food Packaging Processes
8011 aluminum foil can be employed in food packaging.
Some of its food packaging applications are as follows:
Snack and candy packaging
Flexible food packages and bags
Lids for dairy products
Food forming packages and containers
Guidelines in Choosing Thickness
The right thickness to choose is determined according to the application:
Thinner thickness (6-12 microns): Best for composite flexible packaging, when the foil is used as a barrier layer in a multi-layer film.
Thicker thickness (15-30 microns): Required for packaging products like trays, which should have high strength and formability.
How thickness influences foil: Thickness affects the barrier qualities, strength and cost: the thicker the thickness, the better barrier and stronger the foil but higher is the cost.
Required Core Quality and Purchasing Conditions
Manufacturers who buy 8011 foil for food packing should:
Carefully monitor surface imperfections, such as pinholes, oil stains and scratches for proper printing, coatings and lamination process.
Ensure the qualities of the alloy, thickness tolerance, roll quality and delivery protection.
Make sure the foil is food-grade certified and that full traceability documents are available.
Specific Standards for 8011 Aluminum Foil Used in Pharmaceutical Packages
Enhanced Quality Standards
Pharmaceutical products are particularly vulnerable to moisture, oxygen and light.
In terms of barrier performance and stability, pharmaceutical foil is subject to greater requirements than food packaging foil.
Even the slightest alteration in the thickness of the foil or the presence of a pinhole can endanger the stability and effectiveness of the medicine.
Common Types of Compatible Packaging
8011 aluminum foil can be used for:
Pharmaceutics blister packaging (as lidding and forming foil)
Aluminum plastic combined packaging
Pharmaceutical handbag and strip packaging
Can be connected with the coating and lamination technologies for a proper protection in pharmaceutical applications
Key Quality Control Parameters
In regard to pharmaceutical applications, manufacturers have to focus on:
The thickness uniformity: Ensures the stability of barrier functions and sealing.
The minimal number of pinholes: Even one pinhole may result in the moisture penetration into the package making the medicine ineffective.
Surface cleanliness: It is important for a successful application of lamination and printing processes.
Main Differences Between the Aluminum Foil for Food and Pharmaceutical Package Manufacturing
Protocols for Choosing and Acquiring 8011 Aluminum Foil for Food/Pharmaceutical Packing
Specify the Product Requirements as per the Requirement
Check thickness, width, and roll measurements based on the following:
Type of product packing (direct, printing, coating, lamination)
Purpose of the packing and sensitivity of the packed product
Size of machinery in the production line (size of roll diameter, weight and width of roll)
Importance of Stability of the Rolls Required in Larger Quantities
Rolls of aluminum should be of equal quality in thickness, smoothness, and dimensions to have uninterrupted output process.
Quality of the rolls must be stable to decrease the occurrence of downtime and minimize waste of raw materials, which means they are very important for large volume production within the food and pharmaceutical industry.
Basic Criteria for the Aluminum Supplier Evaluation
In the evaluation process, make sure to check the following parameters of the supplier:
Production capacity: will the supplier meet our demands of volume?
Batch stability: does the supplier deliver rolls of the same quality all the time?
8011 Aluminum Foil Roll Applications HTMM provides large rolls of 8011 aluminum foil for food and pharmaceutical packaging companies, as well as flexible packaging suppliers.
Our offerings include:
Custom specifications: Thickness, width, roll weight, and inner diameter customized to meet your production requirements.
Supporting alloys: We not only provide 8011 but also 1235, 3003, and 8079 aluminum foils with respect to different applications.
Bulk orders support: We ensure quality and delivery in bulk orders with all the aspects covered, from alloy selection to roll wrapping.
8011 aluminum foil solution from HTMM is a trusted source of quality, certified safety, and custom specifications required by food and pharmaceutical packaging plants.
Contact HTMM for more information on your specific requirements.